
Precision Metal Stamping Manufacturers for Custom Stamped Parts
Buckeye Shapeform is a metal stamping manufacturer built to give low-to-medium volume programs the same precision and process control as high-volume runs. From tin containers for cosmetics to trays for missile assemblies, every stamped part starts with a die set we design and build ourselves. Our sheet metal stamping service handles thin-gauge aluminum, steel, stainless, tin plate, and soft alloys for customers who need a partner—not just a press.

±0.01
Sheet Metal Tolerance
In-House Since 2021
Full Process Control
4 Materials Stocked
Sheet Metal Tolerance
Zero Tooling Cost
Vs. Punch Press
WHY BUCKEYE
Why Choose Buckeye Shapeform for Custom Metal Stamping

In-House Die Design & Tooling
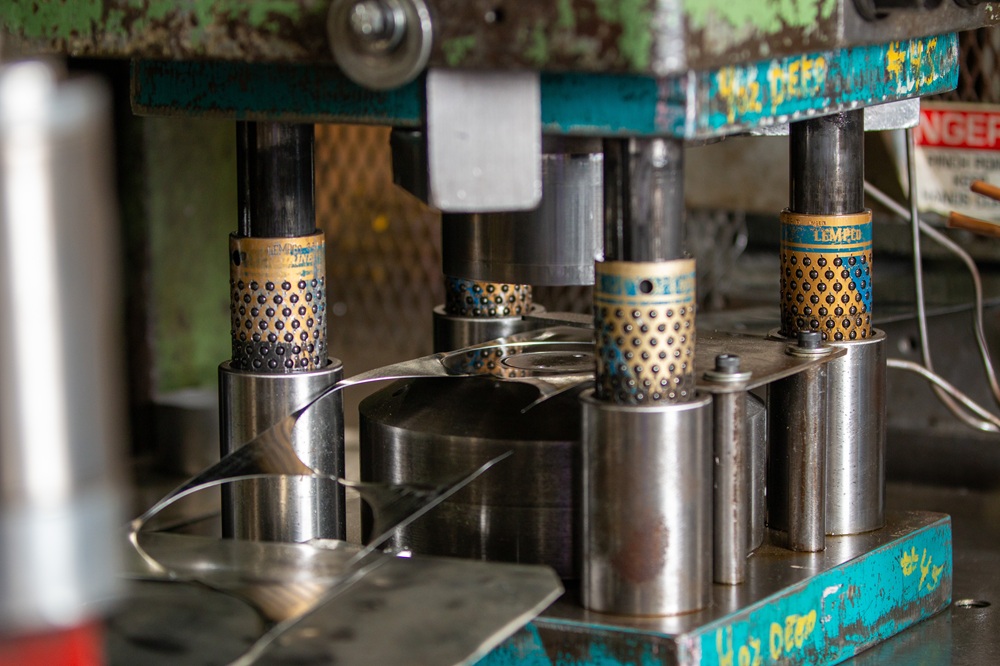
Each part we stamp is backed by tooling built in our own shop, engineered specifically to that part's geometry. We favor simple, single-hit tooling over complex progressive dies, which keeps development straightforward and puts us in control of the schedule from concept to first article.
Built for Small to Medium Orders
We work by the hundreds and hundreds of thousands, not the millions—the volume range automotive-scale stampers are built to skip past. As a stamped metal parts manufacturer sized for this range, we take on programs that don't fit a high-volume shop's minimums.
Material Range for Thin-Gauge Parts
We stamp aluminum, cold-rolled and stainless steel, tin-plated steel, copper, and other soft alloys. Our niche is thin-gauge material, which keeps our tooling and press capabilities matched to what we do best.
CMM-Verified, Die-Maintained Quality
Every run is checked on our CMM equipment, with die sets inspected and maintained between runs. Since punch and die form each part on a one-to-one basis, any non-conformity signals us to stop and inspect the tooling immediately.
Support Throughout the Process
Customers often arrive with a part concept rather than a manufacturable design. Our team develops the process and die design needed to produce it, flagging issues before tooling is cut rather than after.
Everything Under One Roof
From die design through final finishing, we never send a stamped part out to another shop for machining, coating, or assembly. That in-house control is what lets us deliver a fully finished precision metal stamping project instead of a raw stamped blank.
MATERIALS
What We Stamp
PRIMARY
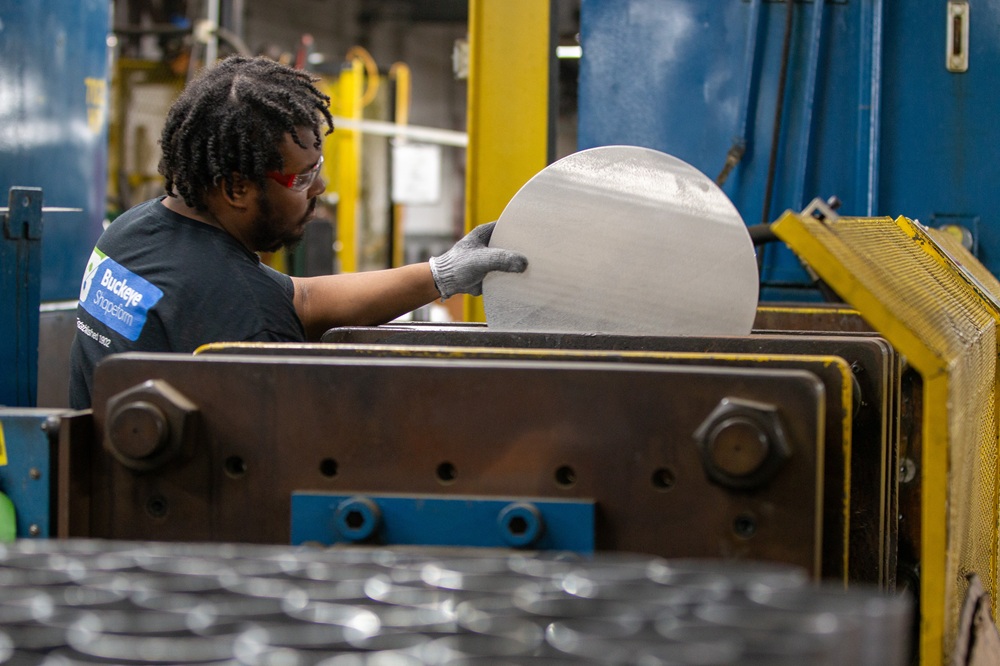
Aluminum
Most common — all standard alloys
COMMON
Stainless
Cold-rolled and stainless steel
COMMON
Steel
Tin-plated steel
COMMON
Copper
Copper and other soft alloys
BY REQUEST
Other Material
Thin-gauge material
INDUSTRIES
Industries We Serve
- Consumer & Packaging
- Defense & Aerospace
- Industrial & Manufacturing
- Electronics & Technology
Frequently Asked Questions About Our Precision Metal Stamping
If you still need an answer to a question that is not covered here, please reach out to us!
How is your stamping process different from progressive die stamping?
We run single-hit tooling, not progressive dies. In a progressive setup, one large die set performs several operations as the material advances through multiple stations—a complex, high-investment approach used mostly for high-volume automotive-style production. Our die sets are simpler: one punch, one die, and one part per cycle. That keeps tooling costs and lead times lower for programs that don’t need progressive die volume.
What materials and thicknesses can you stamp?
We work in aluminum, steel, stainless, tin-plated steel, copper, and other soft alloys, all in thin gauge. Thickness capability depends on the tonnage of the press being used for a given job, since press tonnage determines how thick a material the tooling can push through cleanly. We’ll confirm the gauge and diameter for your specific part during quoting.
How long does it take to develop tooling for a new stamped part?
Design typically takes about two weeks. Building the physical tooling adds another 6 to 8 weeks depending on part complexity and size. Altogether, plan on roughly 10 to 12 weeks from concept to a first physical part, plus time for any adjustments after first-article review.
What production volumes make sense for stamped parts?
Tooling requires a real upfront investment, so the production run needs to be large enough to justify that cost. Our press capacity and die-building process are geared toward the hundreds-of-thousands range rather than dedicated automotive-scale volumes. That focus is what makes our custom metal stamping service a practical option for programs a high-volume shop wouldn’t take on.
Can stamped parts be machined or finished after stamping?
Yes. A stamped shape is often just the first step. We regularly take a stamped blank and run it through CNC machining for tighter tolerances, then apply finishing as needed—the same approach we use on parts that move from a simple stamped tray into a precision-machined component.
How does sheet metal stamping fit alongside your other fabrication capabilities?
Stamping is one piece of a larger in-house process, not a separate service. A part might start as sheet metal stamping, then move to CNC machining before it ever reaches the press. Because every step happens in the same facility, we can sequence stamping with whatever other operations your part requires.
Ready to Get Started?
Bring us your part concept (a drawing, a model, or even a hand sketch) and we’ll walk you through what it takes to tool it, stamp it, and finish it, all in the same facility. Reach out today for a quote.